Vertical Grinding Machine: Built for Parts That Hang Too Heavy
Release time:2026-11-02 Visits:0
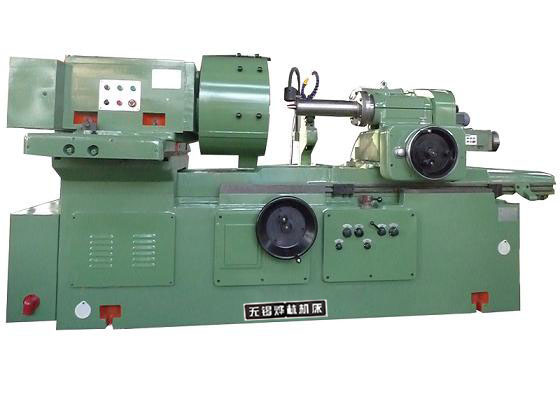
A vertical grinding machine sets the spindle vertical and the worktable horizontal, so the workpiece lies flat on the table instead of hanging off centers or a chuck. The change sounds small. In practice it transforms how heavy disc, ring, and cylinder parts are machined.
This article explains the layout's advantages, the parts it is built for, and the choice between a pure vertical grinder and a vertical turn-grind machine.
Why the Vertical Layout Wins for Heavy Parts
1. Gravity works for you, not against you.
On a
horizontal cylindrical grinder, a 300 kg ring suspended between centers sags under its own weight, and the sag shows up as out-of-roundness. On a vertical machine the part sits flat on the table, supported along its whole face. The load goes into the table bearing, not into the spindle.
2. Rigidity without overbuilding.
The table bearing carries the workpiece directly, so the machine does not need the oversized spindle and tailstock that a horizontal machine needs for heavy work. That is why vertical grinders routinely handle parts from 300 mm to several meters in diameter with better geometry than horizontal machines of the same weight class.
3. One clamping, better concentricity.
Because the part stays flat on the table, its axis is defined by the table rotation. Turning and grinding in the same setup keeps every diameter concentric to the same axis — the classic problem of clamping a heavy ring twice disappears.
4. Easier loading.
Crane the part onto the table, clamp it, done. No balancing between centers, no slinging into a chuck. Setup time drops, and so does the risk of dropping a valuable part.
Parts That Belong on a Vertical Grinder
- Large flanges and rings — pipe flanges, turbine casings, slewing rings, anything too heavy to hang.
- Cylinder liners and sleeves — grind the OD and face in one setup, hold squareness to the bore.
- Large bearings and races — diameters above the practical range of horizontal ID/OD grinders.
- Discs and rotors — brake discs, motor rotors, where both faces must run true to the axis.
- Short, large-diameter parts of any kind — the length-to-diameter ratio is irrelevant because the part lies flat.
Vertical Grinder vs. Vertical Turn-Grind Machine
A pure vertical grinder only grinds. A vertical turn-grind machine adds a turning capability — the table rotates for turning passes, then switches to the grinding spindle for finishing. For parts that need both operations, the combined machine eliminates the second clamping entirely.
The trade-off mirrors every combined machine decision:
|
|
Pure vertical grinder |
Vertical turn-grind machine |
|
Best for |
Parts that arrive pre-machined, grinding only |
Parts needing turning and grinding |
|
Stock removal |
Grinding only (slow) |
Turning removes stock fast, grinding finishes |
|
Concentricity |
Excellent |
Best — single clamping for both ops |
|
Investment |
Lower |
Higher, but replaces two machines |
Medium and large cylinders and conical workpieces are the classic turn-grind case: turn the OD, grind the inner wall, all in one clamping, with the production-line rhythm improving measurably versus two machines and two setups.
Specs That Matter on a Vertical Grinder
- Table diameter — the binding limit for your largest part.
- Max swing and grinding height — tall parts hit the column; check height before diameter.
- Table bearing type — hydrostatic or roller bearings for heavy work; plain bearings sag under load.
- Spindle power and speed — 15 kW and up for production grinding of large diameters.
- In-process gauging — on large expensive parts, in-process measurement pays for itself in one scrapped workpiece.
Common Questions
Q: Can a vertical grinding machine grind bores?
A: Yes. The grinding spindle can be positioned to grind internal diameters and faces, which is standard on vertical turn-grind machines.
Q: What accuracy can a vertical grinder hold?
A: Roundness and flatness in the 0.003–0.005 mm range in production, with better results on rigid machines with hydrostatic tables and careful thermal control.
Q: When should I choose a vertical machine over a horizontal cylindrical grinder?
A: When the part is heavy enough to sag between centers (roughly 100 kg and up, depending on geometry), or when its diameter is large relative to its length. Light, long shafts stay on horizontal machines.
 English