Rotary Table Surface Grinder: The Production Choice for Round Parts
Release time:2026-10-05 Visits:0
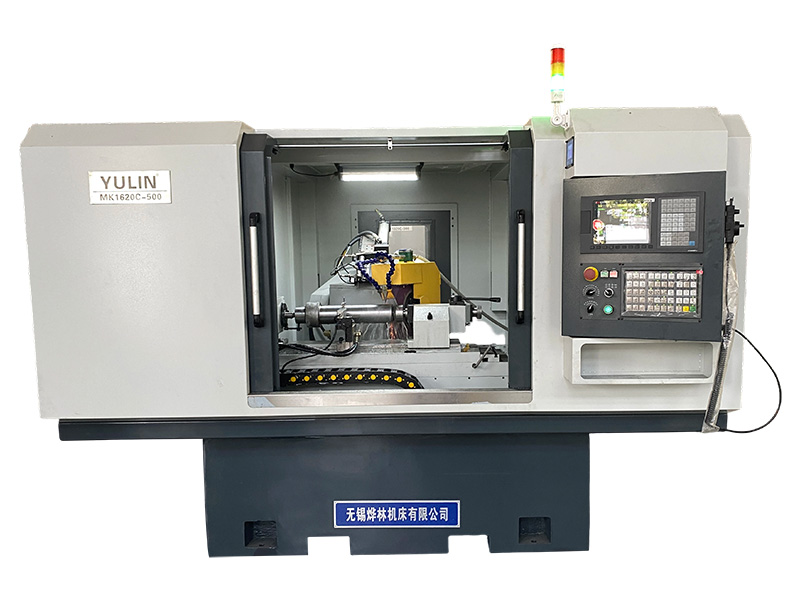
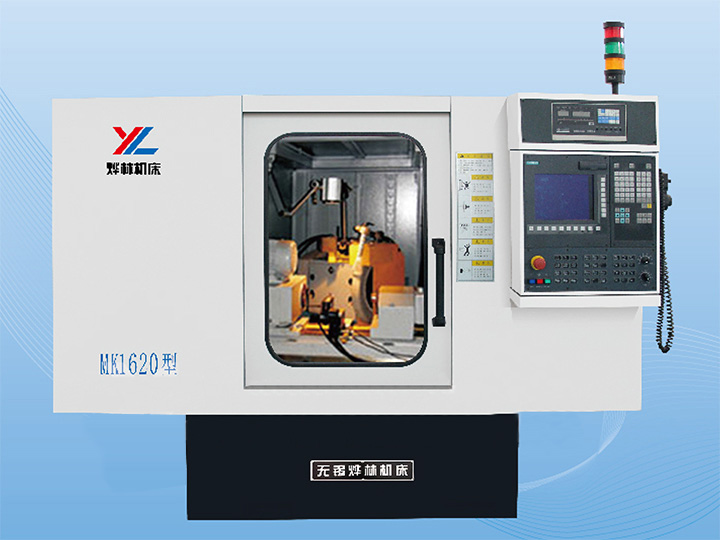
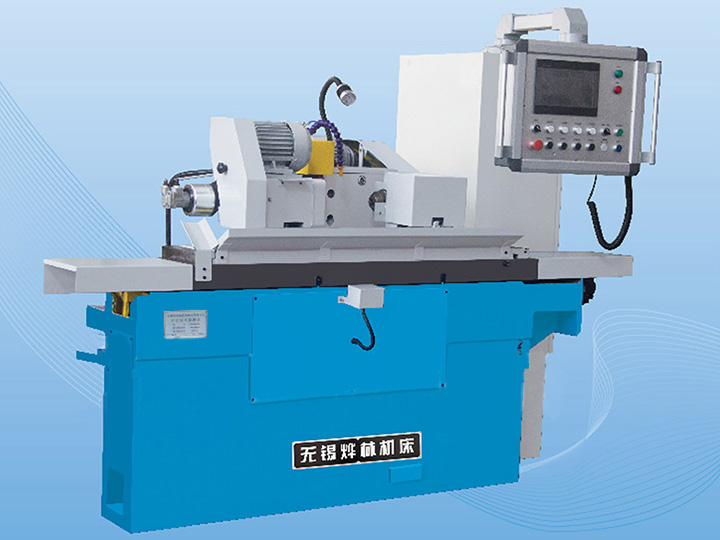
A rotary table surface grinder holds the workpiece on a rotating magnetic chuck while a grinding wheel — usually with a vertical spindle — removes material from the flat face. Because the table rotates continuously instead of shuttling back and forth, the wheel always meets fresh work, and there is no reversal shock to absorb.
For ring-shaped and disc-shaped parts in batch production, this layout routinely out-produces reciprocating surface grinders by 30–50%. This article covers how the machine works, the parts it suits, and what to check before you buy.
How It Works
The machine has three elements you need to understand before comparing models:
- Rotating magnetic chuck — carries the workpiece; rotation speed is adjustable, typically 10–60 rpm depending on diameter.
- Vertical spindle with cup, segment, or ring wheel — the wheel face grinds the full width of the part in one pass; feed comes from the wheel head moving down.
- Automatic down feed — steps the wheel head by a programmed increment after each pass, with spark-out passes at the end for flatness.
Because the table rotates, every point of the part passes under the wheel repeatedly, and the grinding forces cancel around the circle. That is why flatness stays consistent even on thin rings that would distort on a reciprocating machine.
Where the Rotary Table Machine Wins
The layout pays off most on:
- Bearing rings and races — outer and inner rings, thin-section rings that must stay flat after grinding.
- Gear blanks and gears — face grinding before hobbing or shaping, holding the datum face square to the bore.
- Flanges and discs — pipe flanges, motor end bells, brake discs, any round plate needing two parallel faces.
- Short cylindrical parts — piston rings, washers, valve plates, grinding both faces parallel in one setup.
- Roughing castings — with a segment wheel, the machine removes scale and draft quickly before finish grinding.
For rectangular or long parts, a reciprocating surface grinder is still the right tool. The rotary table is a part-geometry decision, not a universal upgrade.
Key Specifications to Compare
When you ask for quotes, line up these numbers side by side:
|
Specification |
Why it matters |
|
Chuck diameter |
Sets the largest part you can grind; leave margin for fixturing |
|
Wheel spindle power |
7.5 kW and up for production; 4 kW is toolroom class |
|
Max workpiece height under the wheel |
Often the forgotten limit — tall parts hit the wheel guard first |
|
Down feed resolution |
0.005 mm for production; 0.002 mm for precision work |
|
Chuck rotation speed range |
Lower speeds for large diameters, higher for small parts |
|
Coolant and magnetic separator |
Decide whether finishes stay stable through a full shift |
Two details deserve special attention. First, the magnetic chuck is the accuracy foundation — a fine-pole chuck is worth the premium if you grind thin rings. Second, automatic dressing with compensation keeps the wheel face flat without stopping production; without it, flatness drifts as the wheel wears.
Production Tips
- Grind in two passes. Rough with a coarse wheel or segments, then finish with a fine wheel. Do not try to do both with one wheel.
- Use spark-out. A few seconds of spark-out after the last feed pass removes most of the spring in the system and measurably improves flatness.
- Check chuck magnetism. Thin parts can lift at the edges during grinding; reduce the chuck speed or use mechanical clamps for parts below 3 mm thick.
- Dress by schedule, not by feel. Log the number of parts between dressings and stick to it. The wheel face condition shows up in the parts before the operator notices.
Common Questions
Q: What is the difference between a rotary table surface grinder and a cylindrical grinder?
A: The rotary table machine grinds flat faces of round parts; a
cylindrical grinder grinds the outside or inside diameters of shafts and bores. They are complementary, not interchangeable.
Q: Can a rotary table surface grinder grind non-round parts?
A: Yes, with fixtures, but throughput falls. Rectangular and strip parts are better on a reciprocating machine.
Q: What flatness can it hold?
A: On a rigid machine with a properly dressed wheel, 0.005 mm over the part diameter is achievable in production, and better with spark-out and fine wheels.
 English