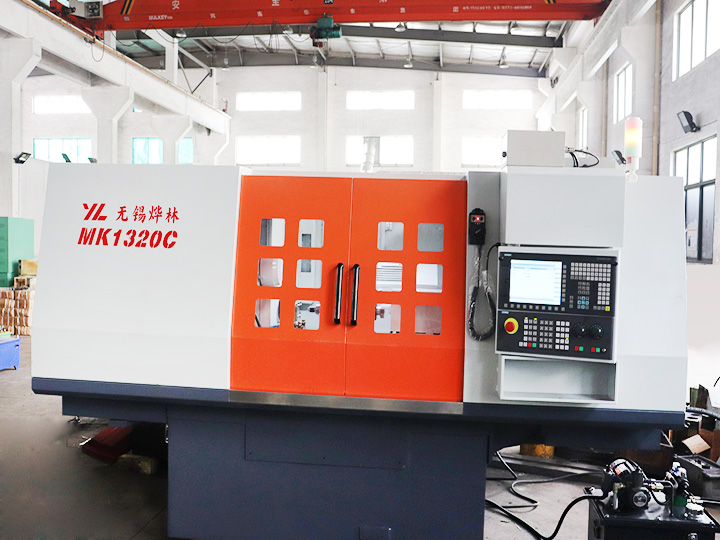
Surface Grinding Machine: What It Does, and How to Pick the Right One
Release time:2026-09-21 Visits:0
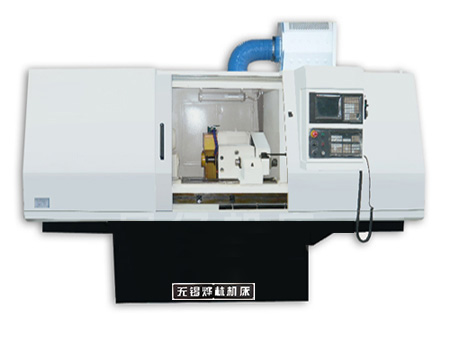
A surface grinding machine removes stock from flat workpieces with a rotating abrasive wheel, leaving a flat, square surface that machining centers and lathes cannot match. It is the machine you reach for when a part needs a datum face, a tight flatness tolerance, or a finish below Ra 0.4 μm before further operations.
This guide covers how surface grinders work, the main configurations on the market, what the specs actually mean, and the mistakes buyers make when ordering their first machine.
How a Surface Grinder Works
The basic cycle is simple: a grinding wheel spins at high speed above a magnetic chuck, the chuck carries the workpiece back and forth beneath the wheel, and the wheel head feeds down a few microns per pass.
Three movements matter:
- Wheel rotation — the cutting motion, typically 28–35 m/s at the wheel periphery.
- Table reciprocation — the longitudinal feed of the workpiece.
- Cross feed and down feed — the positioning motions that set the depth of cut.
What separates a good machine from a cheap one is not the cycle itself but the rigidity and guideway quality behind it. A cast-iron bed with hardened and ground guideways holds geometry pass after pass. A welded sheet-metal bed drifts, and you chase the drift with handwheels all day.
Main Types of Surface Grinding Machines
Horizontal Spindle, Reciprocating Table
The most common layout. The wheel spindle is parallel to the table surface, and the chuck moves back and forth under the wheel. Used for flat blanks, mold plates, gauge blocks, and general toolroom work.
Vertical Spindle, Reciprocating Table
The wheel face (segmented or ring-type) grinds the full width of the workpiece in one pass. Stock removal is aggressive, so this type is common for roughing castings and weldments before finish grinding.
Rotary Table Surface Grinder
The workpiece sits on a rotating magnetic chuck instead of a reciprocating table. Because the table never reverses direction, there is no reversal shock, and the wheel is constantly in contact with fresh work. This makes the rotary table machine the fastest way to grind ring-shaped, disc-shaped, and short cylindrical parts in batches — a key reason it dominates production shops grinding bearing rings, gears, and flanges. See our guide to rotary table surface grinders for the productivity math.
Vertical Spindle, Rotary Table
Combines a vertical wheel spindle with a rotating chuck. Very high stock removal, used for medium and large workpieces where flatness matters more than surface finish.
What the Spec Sheet Really Tells You
When comparing quotes, do not stop at table size and price. Check these numbers in order:
|
Parameter |
What it controls |
What to look for |
|
Table working area |
Max workpiece size |
Leave 20% margin beyond your largest part |
|
Wheel spindle power |
Stock removal rate |
3–5 kW for toolroom, 7.5 kW+ for production |
|
Down feed resolution |
Achievable thickness control |
0.005 mm is minimum; 0.002 mm for precision work |
|
Guideway type |
Long-term accuracy |
Hardened and ground V-and-flat ways over linear rails for grinding |
|
Magnetic chuck type |
Workholding rigidity |
Fine-pole chuck for thin parts; standard pole for general work |
|
Grinding wheel size |
Wheel life and cost per part |
Larger wheels last longer between dressings |
Accuracy claims deserve scrutiny. A realistic figure for a new machine is flatness within 0.005 mm over 300 mm of travel. If a supplier quotes 0.002 mm over a meter, ask how they measured it.
Choosing Between Reciprocating and Rotary Table
The decision is mostly about part geometry and batch size:
- Reciprocating table — rectangular parts, long thin strips, mold inserts, anything with a length-to-width ratio above about 3:1.
- Rotary table — round parts, rings, discs, short shafts, and anything that fits within the chuck diameter. Throughput is 30–50% higher because reversal is eliminated.
If your work is a mix, a universal machine with a swiveling wheel head covers more ground but costs more. Most shops are better served by buying the layout that matches their dominant part family.
Practical Buying Mistakes
1. Oversizing the table. A 500 mm table that runs empty 60% of the time costs more in floor space, coolant, and wheel cost than two smaller machines.
2. Ignoring the chuck. The magnetic chuck is where accuracy is lost. Budget for a quality fine-pole chuck if you grind thin or small parts.
3. Forgetting coolant filtration. Surface grinding generates fine abrasive sludge. A magnetic separator plus paper filter extends wheel life and keeps finishes stable.
4. Buying on horsepower alone. A bigger motor on a flimsy frame just produces chatter marks. Rigidity and damping come first.
Maintenance That Keeps the Machine Accurate
A
surface grinder is only as good as its ways and chuck. Weekly: clean the chuck surface, check the coolant concentration, and verify the wheel is balanced. Monthly: check the parallelism of the wheel head to the table, and scrape or re-grind the chuck if parts no longer hold flat. Annual: full geometry check — table flatness, spindle runout, and squareness of the wheel head to the table.
Common Questions
Q: Can a surface grinder remove a lot of stock?
A: Yes, but it should not. Use a milling machine for stock removal above 0.3 mm per side and the grinder for finishing. Grinding deep cuts wastes wheel and time.
Q: What surface finish can a surface grinder achieve?
A: Ra 0.2–0.8 μm in normal production, and down to Ra 0.1 μm with fine wheels, spark-out passes, and a rigid machine.
Q: Do I need a rotary table or a reciprocating table for round parts?
A: Round parts under 400 mm diameter in batch production belong on a rotary table surface grinder. Long shafts and rectangular plates belong on a reciprocating machine.
 English