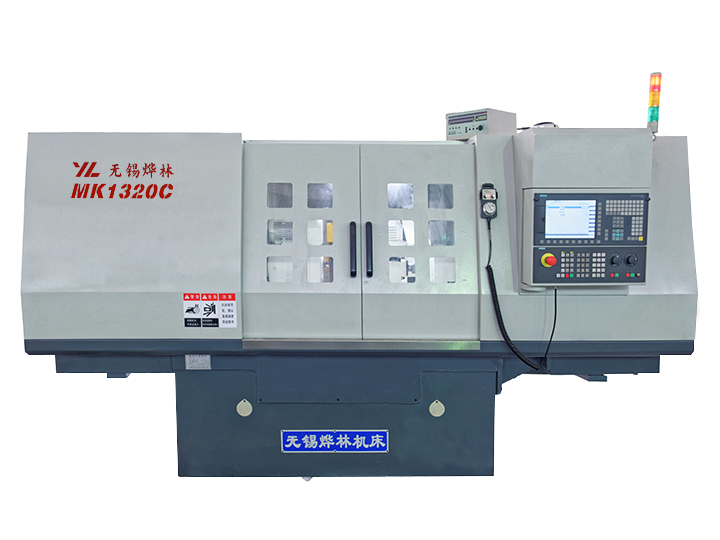
CNC Vertical Lathe: The Machine for Big Round Parts
Release time:2026-11-16 Visits:0
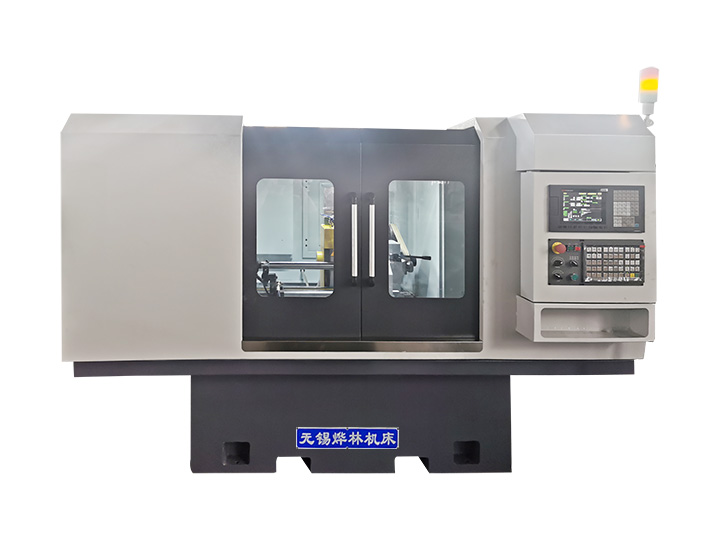
A CNC vertical lathe sets the spindle axis vertical and the worktable horizontal, so large disc, ring, and sleeve workpieces lie flat on the table while a CNC-controlled tool turret machines them. Wind-power components, aerospace rings, shipbuilding parts, and heavy flanges are the machine's natural territory.
The vertical layout exists for one reason: heavy parts should sit, not hang. This guide covers the layout's advantages, the
CNC capabilities that matter, and how to size the machine correctly.
Why the Vertical Layout?
Heavy Parts Sit Flat
On a horizontal lathe, a 500 mm diameter ring clamped in a chuck overhangs the spindle and tries to bend it. On a vertical lathe the part lies flat on the table, supported across its entire face by the table bearing. The table can carry parts weighing several tons without the spindle deflecting — the load goes down through the bearing into the bed, not sideways through the spindle.
Gravity Assists Clamping
Crane the part onto the table, clamp radially or against stops, and go. There is no balancing act, no chuck hanging a heavy part over the operator. Setup for large parts is dramatically faster and safer.
Rigidity That Shows Up in the Parts
The short, stiff load path — table bearing to bed — means chatter resistance and stable machining at heavy cuts. Turning a flame-cut flange with interrupted cuts is routine on a vertical lathe; on a horizontal machine of the same size it is a fight.
What the CNC System Buys You
- Programmed multi-step cycles — rough, semi-finish, finish, with the same feeds and speeds every cycle.
- Taper and profile interpolation — machine tapers, radii, and formed contours without form tools.
- Automatic tool selection — the turret indexes tools mid-cycle; a flange that needs facing, boring, and turning runs to completion untouched.
- In-process measurement — touch probing or gauging corrects for tool wear and thermal drift.
- Integration with MES/ERP — an open CNC control lets production systems feed programs and collect cycle data.
Typical Workpieces
|
Industry |
Parts |
|
Wind power |
Flanges, hub rings, bearing housings, slewing ring blanks |
|
Aerospace |
Engine casing rings, turbine discs, large flanges |
|
Shipbuilding |
Propeller hubs, shaft flanges, large bearings |
|
Heavy machinery |
Gear blanks, brake discs, pulleys, flywheels |
|
Valves and pumps |
Large valve bodies, pump casings, seal rings |
Sizing the Machine
Get these four numbers right and the rest follows:
1. Table diameter — your largest part, plus 10–15% for clamping room. This is the binding spec.
2. Max turning diameter (swing) — overhanging features need swing beyond the table diameter.
3. Max height under the ram — tall sleeves and housings hit the crossrail first; check height before diameter.
4. Table speed range and torque — heavy interrupted cuts need low-end torque, not top speed. Ask for the torque curve, not the max rpm.
Two common mistakes: buying a table too small because the average part is small (the largest part rules), and buying too much speed range while the torque at working rpm is inadequate for the material.
CNC Vertical Lathe vs. Vertical Grinder vs. Turn-Grind Machine
- CNC vertical lathe — removes stock fast with turning tools; the finishing machine for most large parts.
- Vertical grinder — finishing only, for tolerances and finishes turning cannot reach.
- Vertical turn-grind machine — both operations in one clamping; the choice when concentricity between turned and ground features is critical and the part must not move between operations.
Common Questions
Q: How accurate is a CNC vertical lathe?
A: In production, machining tolerance around ±0.01–0.02 mm on diameters is typical, with better results on rigid machines with thermal control. For sub-micron-level geometry, add a grinding pass.
Q: Can a vertical lathe machine small parts?
A: Technically yes, but a horizontal CNC lathe is faster and cheaper for small work. Vertical lathes earn their premium on parts too heavy or too large to hang in a chuck.
Q: What control systems are used?
A: Common choices are Fanuc, Siemens, and GSK-class controls. An open control that supports network program upload and MES integration matters more than the brand if you run a connected shop.
 English